Unstructured Running Caps Factory Guide to Choosing the Right Manufacturing Partner
2026-09-28
Ever received a sample that looked great in photos but fell apart after three washes? That’s what happens when you pick the wrong factory for unstructured running caps. The real difference isn’t in the logo or the color—it’s in how the crown holds its shape and how the seams sit flat against your head. This guide walks you through evaluating manufacturing partners the way industry insiders do, and if you’re ready to skip the trial and error, 4ugear brings the kind of production know-how that turns a good design into a reliable product.
No Buckram, No Structure—But That’s the Point
This book refuses to stand at attention on a shelf. Skip the stiffened cloth, skip the sharp corners that crack instead of bend. What you get instead is a cover that moves with you—rolled into a back pocket, flattened under a stack, opened one-handed on a crowded train. The lack of buckram isn't an oversight; it's an invitation to treat the object less like a monument and more like a tool.
The spine, if you can call it that, doesn't crease so much as memorize. Every fold becomes a soft hinge, every dog-ear a bookmark you didn't have to plan. There's no architecture holding the pages in rigid rows, so the book falls open to the page you've read three times, not the one you're supposed to be on. That looseness is deliberate—a kind of anti-binding that lets the text breathe instead of bracing it for display.
What you lose in durability you gain in intimacy. A paperback without structure doesn't demand a clean desk or a careful hand. It smudges, it curls, it absorbs coffee rings and pencil scratches. And that's exactly the point: this isn't a book to preserve behind glass. It's a book to live with until it falls apart, and maybe a little after.
Sweat, Rain, and the Hidden Cost of Cheap Foam
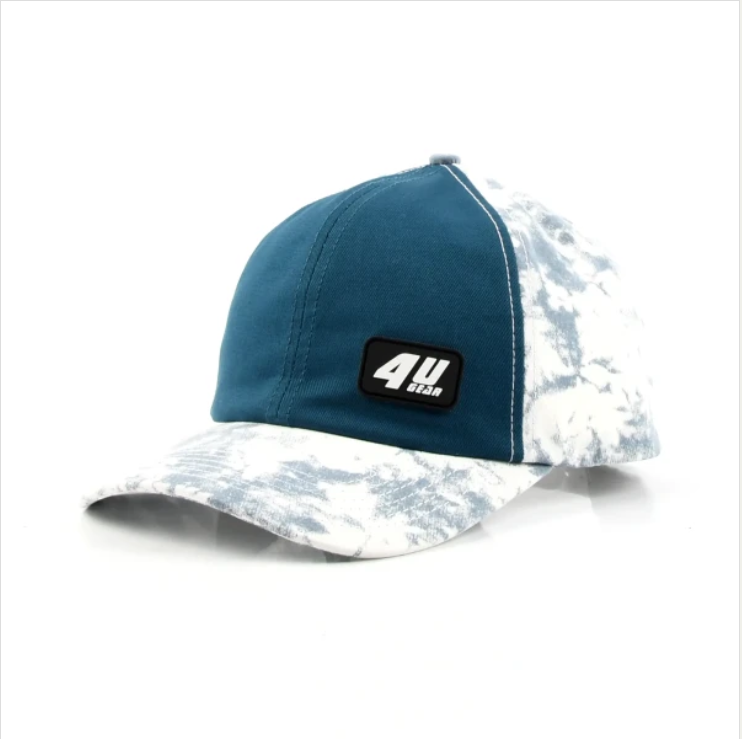
Most people don't think twice about the foam in their running shoes or couch cushions until a humid afternoon turns the material into a sponge. Sweat from a long jog or a sudden rainstorm soaks into cheap polyurethane, and instead of drying out, the foam starts to break down. You notice a sour smell first, then the cushioning flattens in weird spots. What seemed like a bargain starts costing you in replacements, foot pain, or a living room that always smells faintly of mildew.
The real problem isn't just discomfort. Cheap open-cell foam acts like a petri dish once moisture gets trapped. Bacteria and mold thrive in the warm, damp pockets, which can trigger skin irritation or breathing issues you wouldn't link to your mattress or yoga mat. Meanwhile, the foam's chemical structure degrades faster than manufacturers admit, releasing tiny particles that end up in dust around your home. You paid less upfront, but the hidden price shows up in air purifiers, doctor visits, and furniture that's garbage within a year.
There's a reason higher-density or closed-cell foams cost more: they resist moisture instead of absorbing it. Next time you're comparing two similar-looking products, press your thumb into the foam and watch how long it takes to bounce back. If it stays dented or feels damp after a humid day, you're looking at the same cheap stuff that turns sweat and rain into a slow-motion money pit.
Why Factory Samples Always Feel Different Than Bulk Orders
A factory sample usually comes from a different part of the production floor than the bulk run. The person making it is often a senior patternmaker or sample sewer who knows every seam and can ease the fabric by hand; the bulk order, by contrast, gets split across several lines with newer operators, faster stitch settings, and less time for manual adjustments. That alone changes how the fabric settles, how tight the stitching feels, and how the piece hangs on the body.
Then there's the material itself. The sample might be cut from a carefully stored roll or a small batch that was finished by hand, while the bulk order pulls from a newer dye lot or a different supplier run. Even if the mill specs are identical, slight shifts in thickness, grain, or coating will show up in the hand feel. Some samples are also pre-washed or steamed before shipping, whereas the bulk cartons leave the factory straight off the line, so the initial stiffness or sheen can be misleading.
Small-Batch Runs: What Low MOQ Really Costs You
The appeal of a low minimum order quantity is obvious: you don't tie up cash in inventory, you can test new designs without betting the farm, and you avoid the nightmare of a warehouse full of dead stock. But the sticker price on a small run is only part of the story. Once you factor in setup fees, per-unit labor, and the sheer friction of coordinating tiny production batches, that "affordable" pilot order can quietly eat your margin before you've sold a single piece.
Factories often quote low MOQs as a loss leader, but they compensate by pushing material costs up or burying charges in tooling and sampling. You might pay three times the bulk rate for fabric, and then discover that the stitching quality is inconsistent because the line workers are rushing through a job they don't expect to repeat. Every small batch restart means re-explaining specs, re-approving proofs, and absorbing the cost of miscommunication that no spreadsheet line item captures.
The real hidden cost is opportunity. While you're spending weeks managing a 50-unit order, you're not building relationships with suppliers who could give you better pricing at 500 units. And if that small batch finally sells well, you're back to square one, praying the factory hasn't changed its thread color or lead time. Low MOQ feels safe, but it often just shifts the risk from inventory to your own time and repeatability.
Communication Red Flags That Show Up in the First Email
When you open a first email from someone new, a few subtle cues can instantly shape your impression. One of the biggest warning signs is a message that feels like it was copied from a generic template—no mention of your name, your work, or the reason they're reaching out to you specifically. It suggests the sender didn't put in the effort to understand who you are, which often predicts a one-sided or careless communication style down the road.
Another red flag shows up in the tone and structure. An overly stiff, corporate-sounding opening like "Dear Sir/Madam" paired with a wall of text and no clear ask can signal poor social awareness or a lack of genuine interest in a real conversation. On the flip side, an email that's too casual—using slang, emojis, or no greeting at all—might indicate someone who doesn't respect professional boundaries. Both extremes make you wonder whether collaboration will be smooth or exhausting.
Finally, watch for missing information that should be basic in an introduction. If the sender doesn't state their name, their role, or how they found you, you're left piecing together context that they should have provided. Vague requests like "I'd love to connect" without any purpose or next step often mean the person is either disorganized or hoping you'll do the mental work for them. These early signals rarely improve over time, so paying attention to them can save you from a frustrating exchange.
Building a Cap Spec Sheet Your Factory Won’t Ignore
Most cap spec sheets fail because they read like product descriptions instead of production instructions. If your factory has to guess whether the crown height includes the sweatband or whether the brim curve is measured before or after steaming, you have already lost control of the run. Start by pinning down the dimensions that actually change between samples: crown panel width at the seam, total front height from the sweatband stitch to the top button, and the finished brim width at its widest point. Include clear tolerance ranges, not just single numbers, so the line supervisor knows when to stop and call you instead of improvising.
Material callouts matter just as much as measurements. Instead of writing "cotton twill," specify the yarn count, fabric weight after washing, and color code with the exact dye lot reference you approved. List the backing for embroidery or patch placement, the stitch density for the logo, and whether the undervisor needs a contrasting fabric or a moisture-wicking finish. If a trim is sourced locally, name the supplier or attach a photo of the approved sample tag. The goal is to make the sheet impossible to misread from across a noisy factory floor.
FAQ
Ask for a sample run using your exact fabric weight and sweatband material, not their stock sample. A factory that pushes back on this or only shows you photos usually won't match what you need for a soft, bendable crown that keeps its shape when wet. Also ask how they bond the brim and whether they use heat-sealed or stitched seams for the interior, because that's where cheap caps fall apart.
Have them walk you through how they handle the front panel without a buckram backing. Unstructured caps need the fabric itself to hold the silhouette, so the cutting and seam allowance matter more. A factory that talks about 'removing the stiffener' but doesn't mention fabric tension or crown height adjustments probably just makes dad caps and slaps a running label on them.
Look for breathable nylon or recycled polyester with a light mesh lining, and a sweatband that won't get crusty after repeated washes. But a smart factory won't just list materials—they'll ask about your climate and end use, then suggest options like perforated side panels, reflective binding, or a brim foam that doesn't soak up rain. If they don't ask any questions about how the cap will be used, move on.
Not always. Some factories offer 50-piece runs but bury the cost in setup fees or use leftover fabrics. Instead of chasing the lowest MOQ, ask for a transparent cost breakdown: fabric, cutting, sewing, brim forming, and packing. A factory that shows you those numbers and offers a tiered pricing path as you scale is more valuable than one promising tiny runs with no route to growing your margin.
Order a pre-production sample with your logo and request a wash test—three cycles, air dry, then check the brim curve and seam puckering. Then ask for a photo of the sample next to their production line, not just a close-up. You want to see if they have the right machines for soft crowns and flexible brims. If they're stitching everything on standard flatbed machines, the cap will twist when you run.
For a new order with custom fabric, expect 30 to 45 days after sample approval. Anything faster means they're probably using stock fabric or rushing the cutting. Delays usually come from fabric sourcing, not sewing. Ask the factory to send you a weekly photo of your fabric bolt or cutting table—serious partners do this without being asked, and it's the single best way to avoid a 'stitching backlog' excuse later.
They point out problems before you do. A good factory will tell you that your initial brim curve looks off for a size large, or that the reflective thread you chose will crack after twenty washes, and then offer a fix with a cost estimate. That proactive communication is rare and worth more than a low price. Also check if they remember your previous order details without you re-sending specs—that means they keep real records.
Conclusion
Choosing a factory for unstructured running caps means unlearning plenty of assumptions you picked up from structured hats. The absence of buckram isn't a defect; it's the whole reason these caps drape and pack flat, so a partner who keeps trying to add stiffness or "fix" the crown is already showing they don't understand the product. Then there's foam. Cheap open-cell foam soaks up sweat and rain, holds odor, and breaks down after a season, but most buyers don't notice until reviews roll in. Ask about density, closed-cell alternatives, and how the padding behaves when wet—not just how it feels on a showroom sample. And speaking of samples: factory samples always feel different than bulk because sampling lines run slower, use leftover premium fabrics, and get individual attention. If your factory can't explain exactly which variables will shift in production, you're buying a prototype, not a product.
Small-batch runs carry hidden math. Low MOQ might look friendly at first, but setup fees, fabric minimums, and per-unit labor often get buried, so the real cost per cap can double or triple once you add all the line items. A factory that quotes a low MOQ without walking you through those extras is either hiding them or planning to cut corners later. Communication red flags appear quickly—vague replies, delayed answers about tolerances, or a sales rep who says yes to every request but never asks about your end user. If the first email lacks specifics, bulk production won't improve. Finally, build a cap spec sheet that a factory won't ignore: include panel measurements, seam allowances, foam thickness and density, stitch-per-inch counts, and acceptable shrinkage. Not every factory will follow it, but the ones that push back with informed questions are the ones worth keeping.
Contact Us
Contact Person: Tommy
Email: [email protected]
Tel/WhatsApp: 8613546956008
Website: https://www.4ugearsupply.com/