OEM Purlin Roll Forming Machine Company in China Crafting Durable C Purlins
2026-09-14
Behind every sturdy warehouse and industrial shed stands a machine that shapes steel into the backbone of modern construction. If you're sourcing C purlins that must withstand years of heavy load without compromise, the OEM partner you choose matters more than the steel itself. That’s where Beenew, a China-based purlin roll forming machine manufacturer, steps in — not just to supply equipment, but to redefine what 'durable' means on your production line.
Inside the Production Floor Where Precision Meets Heavy-Duty Steel
The first thing you notice on the floor is the smell of hot metal and the rhythmic thump of a 400-ton press. Overhead, a gantry crane glides along its rails, carrying a freshly sheared plate of AR500 steel that still carries the heat from the cutting table. Forklifts with worn tires weave between workstations, but no one rushes. Every movement follows a path that has been repeated thousands of times.
At the center of it all, a fiber laser traces a pattern through half-inch plate with a hiss that rises and falls. The cut edge glows orange, then cools to a dull gray. Nearby, a machinist checks a bore diameter against a calibrated gauge, jotting the measurement on a clipboard without looking up. There's no tolerance for "close enough" here. When a dozer blade or excavator bucket depends on a mounting bracket, a few thousandths of an inch decide whether it fits the first time or fails in the field.
Heavy-duty steel doesn't forgive mistakes. A misplaced weld on a high-stress joint can crack under load, so each seam is inspected before it leaves the bay. Ultrasonic testers slide over the surface while welders pull their hoods back and watch the screen. The result is a floor where pride isn't talked about—it's measured, tested, and stacked by the loading dock waiting for the next truck.
How Raw Coil Turns Into Load-Ready C Purlins
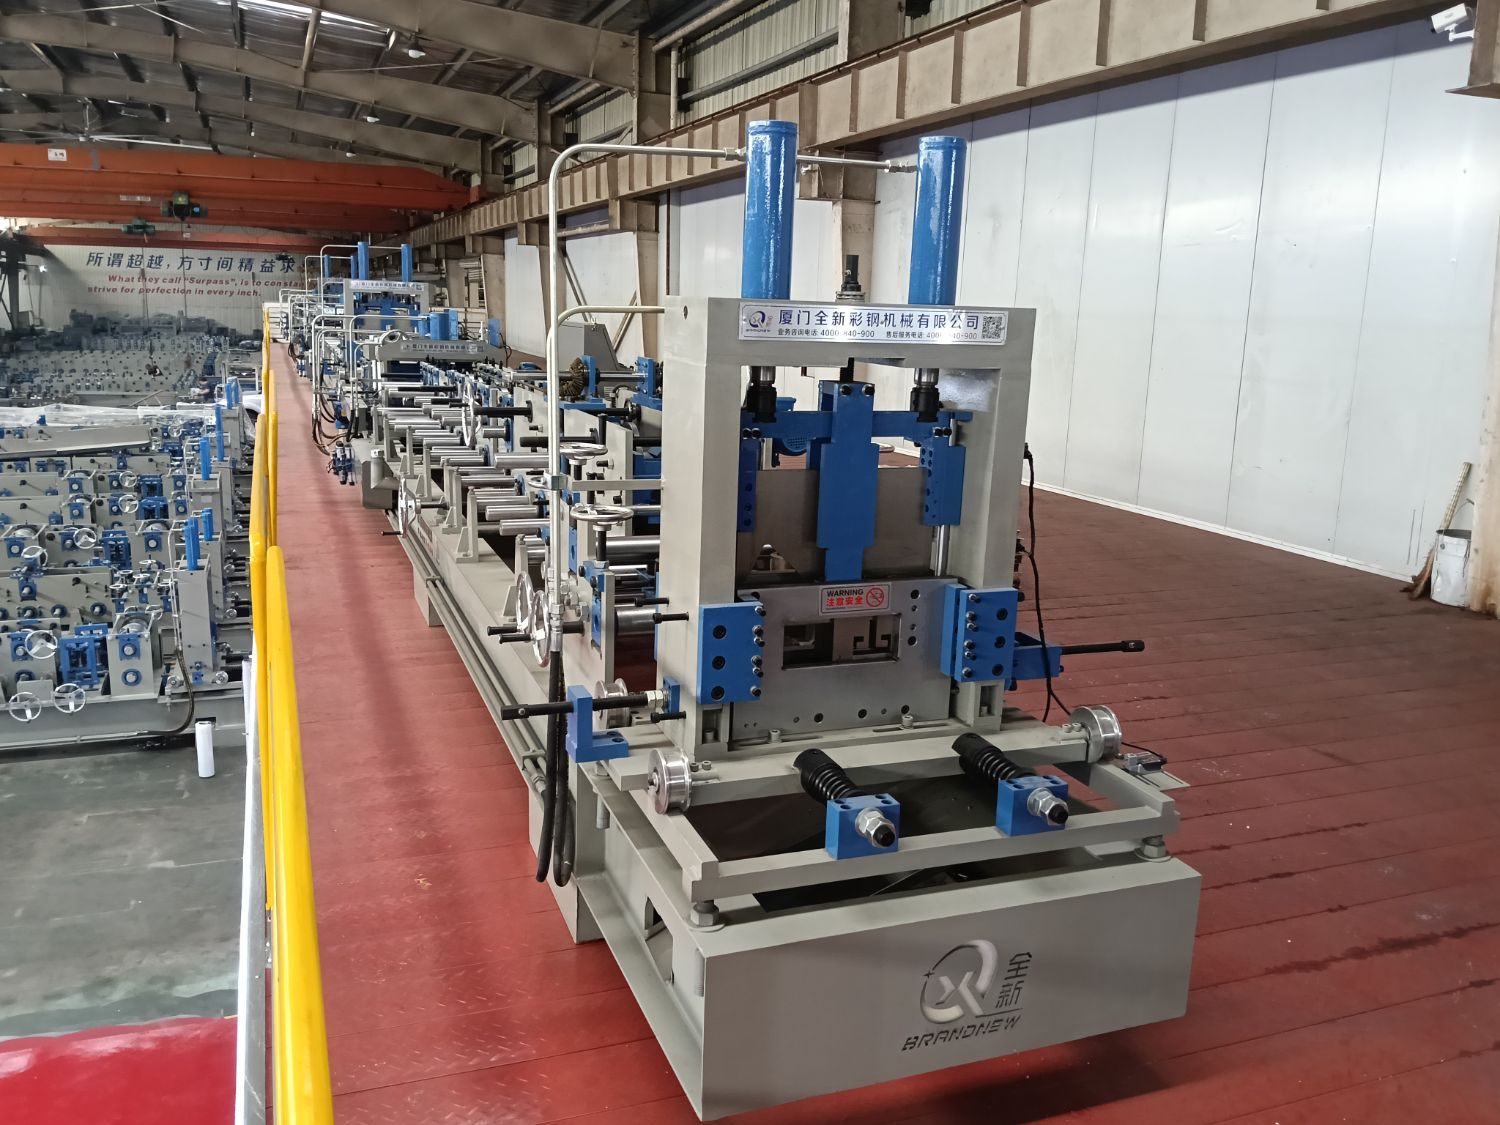
A coil of galvanized steel arrives at the roll forming line looking like a giant silver pancake. It gets loaded onto a decoiler, which feeds the strip through a straightening machine to remove the natural curve and any minor waves from the coiling process. From there, the flat sheet passes into a pre-punching station where holes for bolts, braces, and end laps are pressed out while the steel is still straight—far more accurate than trying to drill after forming.
Next, the strip runs through a series of rollers arranged in consecutive stands. Each stand performs a slight bending action, gradually shaping the flat steel into the familiar C profile with a flat web, two vertical flanges, and short return lips on the top edges. The rolling process is cold, so no heat is applied; the material keeps its zinc coating intact and gains extra rigidity from the work hardening of the bends. At the final stand, the profile is precisely measured by an inline gauge, and any deviation beyond half a millimeter triggers an automatic correction.
After the profile exits the roll former, it moves directly to a flying cutoff saw that slices it to the exact length ordered—no separate measuring or manual cutting needed. The cut piece lands on a run-out table where an operator checks the key dimensions and edge quality, then stacks it into a bundle. At this point, the C purlin is load-ready: uniformly shaped, correctly punched, and protected against handling damage for transport to the construction site.
Engineering the Roll Forming Line for Repeatable Profiles
Getting a roll forming line to spit out the same profile every single time comes down to how well you lock in the tooling setup. Most shops chase their tails because they allow tiny shifts in roll gaps or misalignments between stands to creep in over a long run. We stopped relying on hand measurements and switched to laser alignment jigs that sit on the mill bed before any coil is loaded. That one change cut our dimensional drift by more than half, simply because we stopped guessing at stand-to-stand parallelism.
Beyond alignment, the material itself is the quiet variable nobody wants to talk about. A coil that varies in thickness by a few thousandths or has inconsistent yield strength will produce a profile that looks fine at the cutoff but won't fit the customer's fixture later. We now enforce a tighter tolerance window on incoming strip and run a short trial section at the start of each shift to map how the line responds to that specific heat number. It adds fifteen minutes to setup, but it eliminates the afternoon of sorting parts that used to follow every coil change.
Finally, repeatability isn't just about the steel and the stands; it's about how the line reacts under load and speed changes. We instrumented the entry and exit guides with simple digital indicators that feed into a small display at the operator station. Instead of waiting for a bad part to appear, the operator can see a gradual trend in guide pressure or a slow shift in flange height and make a tiny correction before the profile goes out of tolerance. That closed-loop approach, even without a full CNC retrofit, keeps a twenty-year-old line holding plus or minus ten thousandths on a daily basis.
Why Material Thickness and Yield Strength Dictate Longevity
Take two sheets of steel, both stamped from the same mill order but separated by three-tenths of a millimeter. The thinner one buckles under a load the thicker one shrugs off, and neither shows a crack until years later. Thickness resists bending moments and spreads stress over a larger cross-section, so fatigue cycles that would tear a slim panel simply never reach critical intensity in a beefier one. But thickness alone is a lazy shortcut. Combine it with yield strength—the point where elasticity gives way to permanent set—and you get the real story of how long a part survives before the first micro-fracture appears.
A low-yield material may be thick, yet it dents and deforms under everyday impacts, accumulating plastic strain that accelerates crack nucleation. Conversely, a high-yield steel can be thinner and still stay within the elastic range longer, but too thin and it becomes vulnerable to buckling and corrosion pitting. The sweet spot lives in the interplay: enough cross-section to keep bending stress low, and enough yield strength to prevent the sort of microscopic yielding that eats away at fatigue life. Designers who chase one number while ignoring the other end up with parts that look robust on a spec sheet but fail early in the field.
In real service, corrosion, temperature swings, and repeated loading conspire against both properties. A thick panel resists punctures and rust-through long after a thin one has perforated, while a high yield strength delays crack initiation but can also make the material more notch-sensitive once a crack starts. That's why longevity isn't about picking the thickest or the strongest plate—it's about matching thickness and yield to the actual stress environment, leaving enough margin so that decades of minor abuse never push the material past the point where small defects become unstoppable cracks.
Custom Capabilities That Go Beyond Standard Dimensions
Standard off-the-shelf dimensions rarely line up with the way real rooms behave. An alcove that's 92 cm deep doesn't care that catalog shelves stop at 80 cm, and a sloped ceiling won't adjust itself for mass-produced cabinetry. Custom capabilities let you move beyond those fixed increments by specifying not just length, width, and height, but also clearance, projection, and load distribution. It's a shift from picking the closest match to building around the actual space.
The more interesting side of custom sizing shows up in details you don't immediately see. A longer span might require a thicker core or a hidden stiffener to avoid sag. An oversized panel may need a different edge treatment so it doesn't warp with seasonal humidity changes. These aren't extras bolted on after the fact; they're part of the same dimensional conversation, folding material behavior and joinery into the measurements themselves.
Working this way also changes the sequence of design. Instead of starting with a catalog and hoping the room cooperates, you begin with the room's constraints—sightlines, door swings, how far you can comfortably reach—and let the final dimensions come out of that. The result tends to feel less like an adaptation and more like the piece was always meant for that exact spot.
Field Performance Insights From Structural Contractors
Structural contractors often see a gap between design assumptions and actual field conditions. Rebar congestion at beam-column joints, for instance, routinely forces crews to re-sequence placement or modify splice locations. These aren't failures of the drawings but a reminder that shop-level clarity doesn't always survive first contact with embedded conduits and anchor bolts.
Concrete mix behavior in hot weather remains a recurring concern. Contractors report that slump retention can shift by mid-pour, especially when transit times exceed 45 minutes. Some crews now pre-wet forms and stagger delivery intervals rather than relying solely on admixtures. This practical adjustment has cut down cold joints on longer walls.
Steel erection tolerances also draw steady feedback. Field measurements from multiple projects show that cumulative beam camber can vary enough to affect deck bearing, even when individual members meet code. The fix isn't tighter shop tolerance but earlier communication on erection sequence so any required shim packs or trim cuts are planned, not improvised.
FAQ
We focus on frame rigidity and precise roller alignment so the C purlins come out with consistent dimensions and minimal twist. Many clients notice the difference in how smoothly the material feeds, even at higher line speeds.
Absolutely. We routinely adapt punching units, flange heights, and lip dimensions to match your drawings. Send us a sample or CAD file and the engineering team will confirm the feasible tolerances before production.
Durability starts with the forming process. By controlling the bend radius and avoiding overworking the steel, we preserve the galvanized coating and reduce micro-cracking. We also offer optional inline embossing or stiffening ribs for extra load-bearing capacity.
It depends on the complexity of the tooling and automation level. A standard C purlin line with manual decoiler usually leaves our factory in 35-45 days. Fully automated systems with stackers and servo punching can take 60-75 days.
Yes, we can send technicians to your location for mechanical setup, electrical commissioning, and hands-on training. We also supply detailed manuals and video call support so your maintenance team can handle daily adjustments confidently.
Most of our C purlin lines handle galvanized or cold-rolled steel from 1.5 mm to 3.5 mm thickness, with yield strengths up to 550 MPa. For thicker or high-tensile materials we can upgrade the drive system and roll stations.
Yes. Our quick-change cassette system lets you swap profiles in about 20-30 minutes per station. You can store multiple cassettes for different web heights and flange widths, which is useful for construction suppliers with varied orders.
We keep a stock of commonly worn components like rollers, cutting blades, and sensors. If a part is not in stock, we can usually ship it within 7 days. Remote diagnostics via video or photo sharing often solve issues without waiting for a site visit.
Conclusion
Walking through the production floor of this Chinese OEM purlin roll forming machine maker, you quickly notice that heavy-gauge steel isn't just fed into the line—it's guided, measured, and shaped with a level of repeatability that usually belongs to smaller precision parts. Raw coil enters one end, passes through a sequence of stations where each roller pair bends the profile a few degrees more, and exits as a load-ready C purlin without any secondary straightening. The engineering behind the roll forming line is tuned so that the same profile repeats within tight tolerances, even across different batches and shifts.
Longevity, however, is decided long before the first bend. Material thickness and yield strength are matched to the intended span and load, and the company doesn't push a one-size-fits-all schedule. Contractors who have used these purlins on warehouses, mezzanines, and agricultural buildings report that the lips and flanges hold their shape under real wind and snow loads, with fewer callbacks for twisted or sagging runs. Custom dimensions, hole patterns, and notch placements are handled as standard discussions rather than special exceptions, which means a structural engineer can specify what the job actually needs instead of adapting a catalog size. That practical flexibility—combined with disciplined production—explains why these C purlins show up on sites where failure isn't an option.
Contact Us
Contact Person: Sophie
Email: [email protected]
Tel/WhatsApp: 8615959271231
Website: https://www.beenew-rollformer.com/