Louver Damper Valve Factory Insights for Smarter Industrial Ventilation
2026-11-18
Most ventilation specs look fine on paper—until airflow, pressure drop, and leakage start fighting each other in the field. Louver damper valves rarely get the attention they deserve, yet they quietly decide whether an industrial ventilation system runs efficiently or bleeds energy. We went inside THT's factory to see how these components are actually built, tested, and tuned for demanding environments. Here’s what smarter industrial ventilation looks like before it ever reaches your ductwork.
Blade Geometry Choices That Lower Pressure Drop
A good starting point is to move away from a straight radial stacking line. Adding tangential lean near the hub and tip shifts high-momentum fluid into the endwall corners and alters the radial pressure gradient that normally drives low-energy flow across the passage. The result is a thinner endwall boundary layer and a weaker corner separation, which shows up as a measurable reduction in total pressure drop at part load. On transonic blades, sweep can be used more selectively: pulling the leading edge aft near the tip softens the pre-shock diffusion and moves the shock foot away from the suction surface, so the pressure rise through the shock is less likely to separate the boundary layer.
Leading edge shape has an outsized influence for such a small part of the chord. A slightly elliptical or super-elliptic leading edge, rather than a simple circular arc, clips the suction spike and distributes acceleration over a longer arc. That matters because a sharp local suction peak can trip transition earlier and enlarge the turbulent wetted area. Pairing the blunter nose with an aft-shifted maximum thickness keeps the forward diffusion gentle, while a controlled rear camber recovers pressure over the back half of the chord without inviting open separation near the trailing edge.
Losses in the last few percent of chord are easy to overlook. Reducing trailing edge thickness, or beveling the pressure side so the wake has a shorter base region, lowers the mixing loss that appears immediately downstream. Add a small fillet at the hub and tip junctions and the corner vortex weakens enough to reduce the blockage the downstream blade rows have to digest. These are not dramatic changes, but together they lower pressure drop without forcing a compromise on blade count or throat area.
Reading Tolerance Data From the Damper Assembly Line
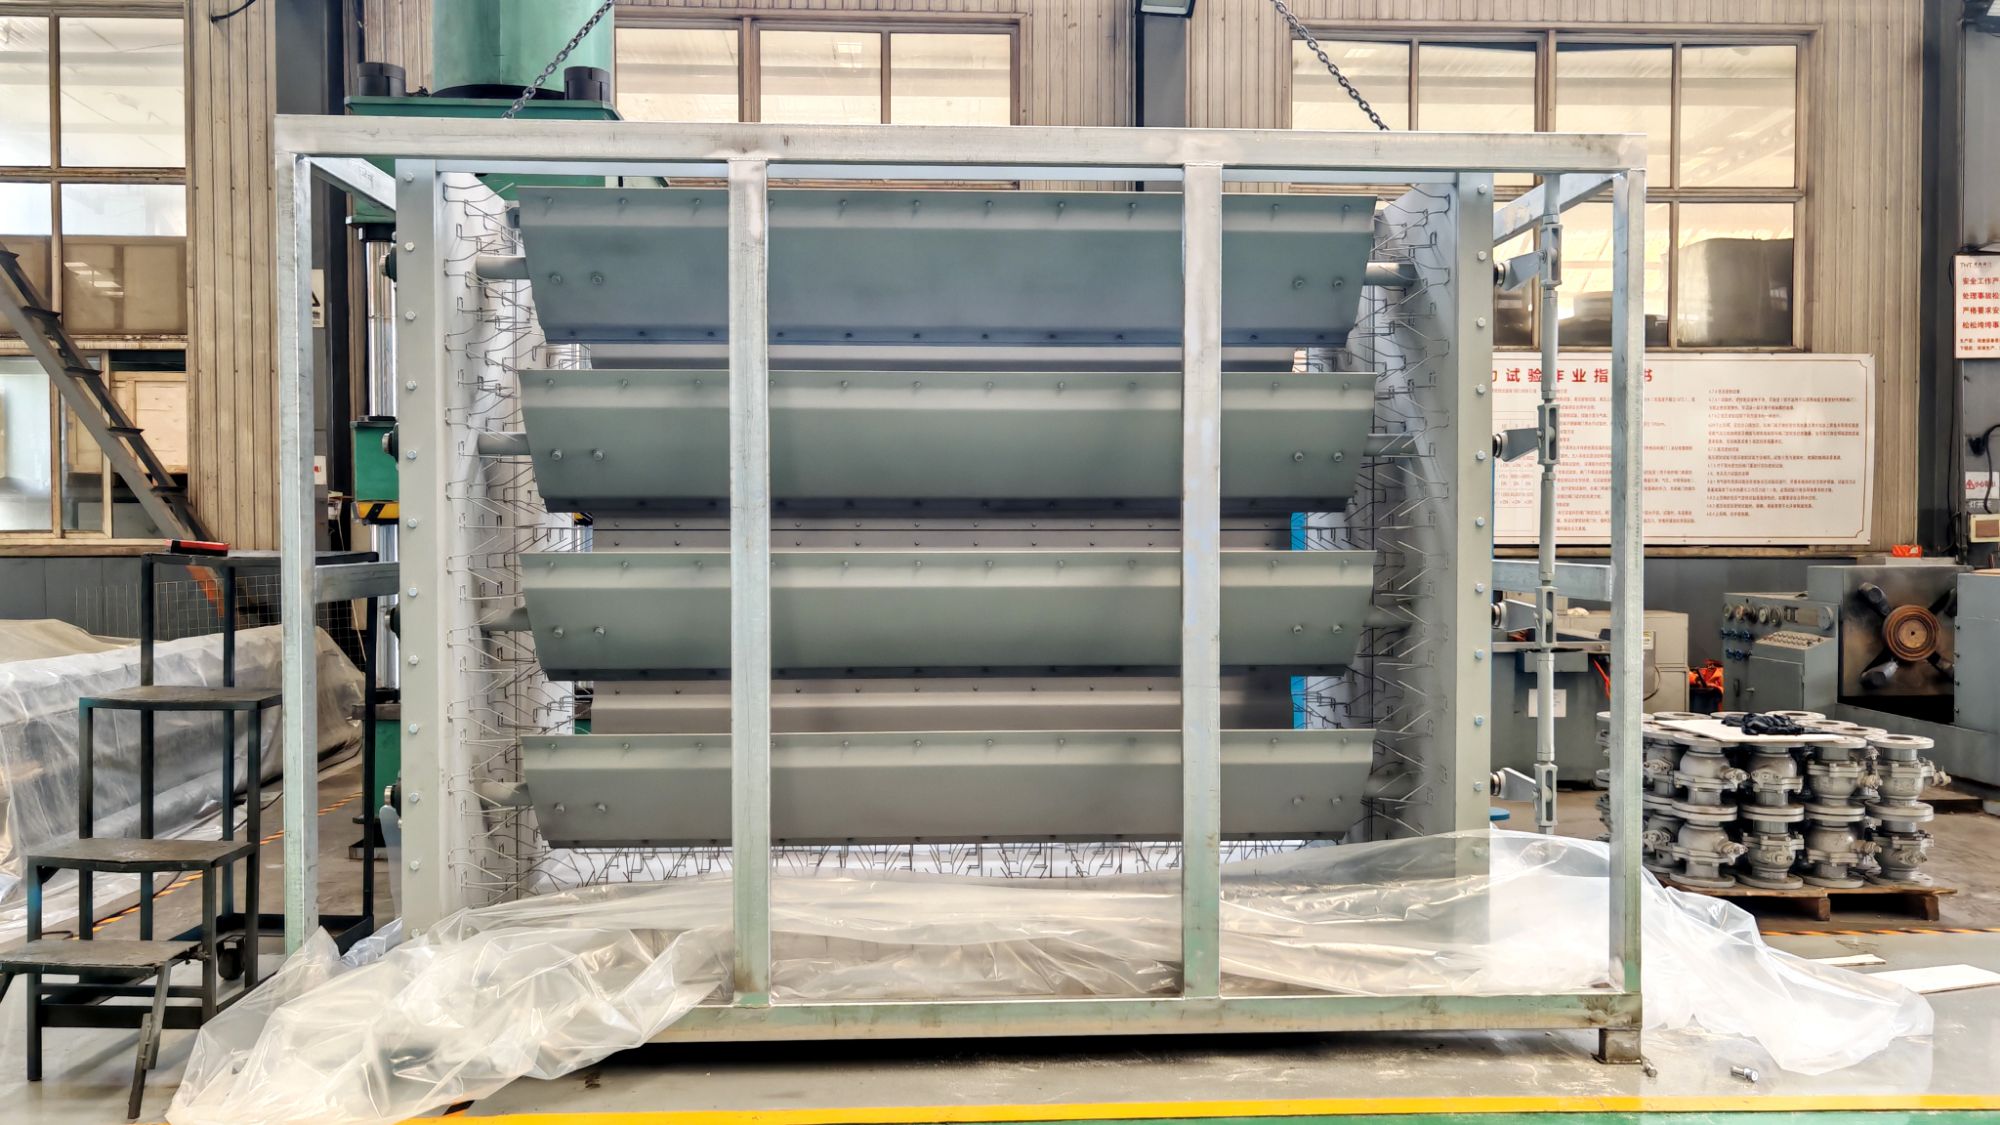
On the floor, tolerance data comes off the damper line in a steady stream rather than as a single clean readout. Operators watch the gauges for patterns: a slight drift across the morning shift often means a fixture has warmed up, while a sudden jump usually points to a misloaded part or a worn contact tip. The numbers themselves matter less than how they move against the last few runs.
Each damper gets checked at the points where small variations tend to show up first, and those readings are logged against the batch, not just the part number. When the same offset repeats on three or four consecutive units, it is treated as a process signal rather than background noise. That distinction helps the line avoid chasing every minor fluctuation and keeps adjustments limited to real changes.
Once the data is pulled into the quality review, it gets compared with the incoming material lot and the tooling schedule. A tight cluster that shifts by half a thousandth can be traced back to a new coil of tubing or a freshly dressed seal seat. Reading the tolerance data this way turns it from a pass/fail gate into a running account of what the assembly process is actually doing.
Actuator Selection Beyond Torque and Voltage Ratings
Torque and voltage figures on a datasheet rarely tell the full story, especially once the actuator is asked to hold position, reverse frequently, or run near its thermal limit for long stretches. A motor can easily satisfy a peak torque calculation yet still struggle in service if the winding insulation is marginal, the thermal time constant is short, or the duty cycle pushes continuous losses well beyond what the frame can dissipate. Paying attention to thermal resistance, ambient temperature derating, and the actual speed-torque curve under load often prevents a costly oversizing or an early field failure.
Mechanical factors also carry more weight than the headline numbers suggest. The reflected inertia of the load relative to the rotor inertia shapes settling time, overshoot, and the ease of tuning; a poor inertia match can make even a high-torque actuator feel sluggish or unstable. Backlash, torsional stiffness, and bearing preload influence repeatability and long-term drift, while radial or axial loading from misalignment can shorten bearing life far more than the rated torque would imply.
The drive and feedback chain deserve equal scrutiny. Bus voltage, current-loop bandwidth, and the resolution of the position sensor affect low-speed smoothness, audible noise, and the ability to correct small disturbances without hunting. In many cases a modestly rated actuator paired with a well-matched drive and a high-quality encoder will deliver better real-world performance than a larger motor that looks stronger on paper but is awkward to tune, noisy at low speed, or poorly supported by its control electronics.
Seal Materials That Stand Up to Thermal Cycling
Seals rarely fail from a single high-temperature spike. They fail because repeated expansion and contraction slowly chews away the material's ability to recover. A seal that holds a static rating at 300°C can still leak after a few hundred cycles if its compression set climbs or the jacket separates from the core. In thermal cycling, the useful question is not just what the temperature limit is, but how much residual load the material keeps after the twentieth or two-hundredth cycle.
Flexible graphite and reinforced PTFE tend to survive broader swings because they tolerate temperature mismatch without stiffening into a brittle lip. Perfluoroelastomers are expensive, yet they hold elasticity and resist hardening across ranges that would turn standard FKM into a cracked ring. For fast cycles, metal-jacketed and spring-energized designs often beat homogeneous elastomers because the spring maintains contact as housing faces shift.
The safest approach is to test a candidate seal the way it will actually be used: cycle it, cool it, heat it again, and measure leakage after the thermal history instead of after initial installation. Pay attention to hardness change, stress relaxation, and the coefficient of thermal expansion between the seal and the groove. A material that simply survives a high oven temperature is not the same as one that can keep sealing when the temperature swings through that range every few minutes.
Custom Flange Details That Prevent Duct Leakage
Leaks in ductwork rarely start in the middle of a straight run. They almost always begin at the joints, where flanges meet and the system depends on gaskets, bolts, and alignment to hold pressure. Custom flange details address this by matching the flange profile to the actual operating conditions rather than relying on a catalog standard. This means adjusting corner radii, adding reinforcing bars where vibration is expected, or specifying a wider sealing face for ducts that carry hot, oily air. When these details are planned during fabrication, the result is a joint that stays tight long after standard options would have started weeping.
One practical approach is to machine matching grooves into both flange faces so the gasket sits in a controlled channel instead of being squeezed unevenly by bolt tension alone. Another is to stagger the bolt pattern on rectangular flanges, placing fasteners closer together near the corners where deflection tends to open the seal. For high-pressure systems, a double-row gasket arrangement with a test port between the rows lets maintenance crews verify seal integrity without opening the duct. These are not one-size-fits-all fixes; they depend on duct size, pressure class, and whether the system handles abrasive particles or sticky fumes.
Fabricators who build custom flanges also pay attention to surface flatness after welding. Heat distortion can leave a flange face slightly convex, which compresses the gasket at the edges but leaves the middle barely touched. A light post-weld skim pass or a controlled flattening step removes that problem before the duct ships. Combined with the right bolt torque sequence and a gasket material rated for the actual temperature swings, these small manufacturing choices make the difference between a duct that holds its first pressure test and one that needs constant retightening in the field.
In-House Airflow Testing Before Products Leave the Floor
Every unit that comes off our assembly line gets connected to a dedicated test duct before it gets packed. Technicians log static pressure, airflow volume, and motor draw at several operating points, then compare those numbers against the build sheet for that specific model. If a fan or blower falls outside its expected curve, it is pulled aside and reworked on the spot rather than shipped and discovered later in the field.
The test bay itself is calibrated each morning, and the instruments are checked against reference orifices so the readings stay repeatable week to week. This matters most on custom orders where a slight change in wheel trim, inlet cone clearance, or housing design can shift performance enough to hear in a duct run.
What leaves the floor is a unit that has already been run, measured, and signed off by the person who built it. That sign-off is attached to the serial number, so when a customer calls with a question months later, we can pull the original airflow data instead of guessing.
FAQ
Blade edge seals, frame rigidity, bearing material, and actuator mounting alignment matter more than catalog pressure ratings. Check continuous welds, blade closure tolerances, and whether coatings are applied evenly across internal surfaces.
Factory-matched linkage and limit switches remove much of the field tuning burden. Blade travel and torque are already set to the actuator, so crews are not repeatedly opening and closing the assembly to chase mid-stroke binding.
Flutter often comes from blade profile or spacing that creates flow separation under pressure. A factory should be able to share open-close behavior at multiple pressure differentials rather than citing only the maximum rating.
Streamlined or symmetric airfoil blades tend to produce a more linear response at partial openings than flat plates. That helps control loops stay stable and avoids sudden flow changes in the low-flow range.
Interface adapters and drilling templates allow existing ductwork to accept dampers with position feedback. This approach reduces downtime and preserves upstream duct sections that are still structurally sound.
Stainless bearings and linkages pay off when the airstream carries moisture, corrosive gases, or frequent washdown cycles. In dry and clean air, the added material cost may not translate into longer service life.
Rising actuator torque, metallic scraping during blade movement, loose linkage points, or localized corrosion are all signs that the assembly needs scheduled downtime inspection rather than another round of lubrication.
By calculating load distribution across each blade and adjusting link length and pivot placement, a factory can keep all blades moving in sync without overstressing one side. This reduces deflection and leakage over years of cycling.
Conclusion
Walking a louver damper valve line, the first thing that stands out is how small shifts in blade profile change the whole ventilation picture. Slightly curved leading edges and tighter chord spacing tend to keep turbulence lower than flat stamped blades, and that shows up as a measurable pressure drop improvement rather than a catalog claim. The assembly data matters just as much: when bore alignment drifts by a few thousandths, torque readings climb even if the parts still pass a basic go/no-go check. Matching actuators to the valve means reading those numbers alongside ambient conditions, because a unit sized only by voltage and torque can struggle once temperature swings tighten clearances. Seal selection follows the same logic. Extruded silicone may look fine on a bench, but repeated thermal cycling often exposes compression set that nobody catches until field leakage appears.
On the fabrication side, custom flange details are rarely about the flange itself. Most leaks trace back to how the gasket face interacts with duct movement, so factories that machine mating surfaces after welding tend to ship fewer problem joints. Before anything leaves the floor, in-house airflow testing closes the loop. A quick damper stroke under no load proves little; running it against a calibrated duct with actual pressure differentials reveals flutter, leak paths, and actuator hunting early. These are not exotic fixes. They are the kind of shop-floor observations that make ventilation equipment behave predictably once installed.
Contact Us
Contact Person: Su Zhang
Email: [email protected]
Tel/WhatsApp: +86-25219206
Website: https://www.tht-valve.com/