China Shell Mold Casting How It Delivers Precision and Cost Efficiency
2026-10-06
You might assume high-precision casting comes with a premium price tag. But in China's shell mold casting sector, that assumption rarely holds. At Zhaoyuqi, precision isn't an upgrade—it's the baseline. The question isn't whether it's possible, but how it manages to cut costs while tightening tolerances. Let's break down the mechanics and economics behind this quietly efficient process.
Where Shell Mold Precision Actually Comes From
Precision in shell molding doesn't start with the mold itself. It begins at the pattern, where thermal expansion allowances are built into the dimensions long before any sand touches resin. If that compensation is off by even a fraction of a millimeter, every downstream step just amplifies the error.
The real source of repeatability is the way the sand-resin mixture cures against a heated pattern. The thickness of that first shell layer, the dwell time, and the cure temperature all interact in ways that are rarely documented. Shops that hold these variables in a narrow band tend to produce castings that need almost no post-machining adjustment.
But the least appreciated factor is the balance between shell permeability and rigidity. A shell that breathes too easily will flex under molten metal pressure, shifting dimensions during solidification. A shell that is too dense traps gas and causes surface defects. Getting that balance right is what separates a good shell mold from one that merely looks accurate.
Why Chinese Foundries Price Below Western Shops Without Cutting Corners
Chinese foundries often charge 20 to 40 percent less than Western counterparts, and the assumption is that lower price means lower quality or hidden shortcuts. In practice, the gap comes from structural advantages: lower labor costs, integrated supply chains, and state-backed infrastructure that reduces capital expenses. When a Shenzhen shop quotes $2.50 for a board that a German shop prices at $4.80, the difference isn't in the copper weight or the solder mask—it's in the cost of running the factory itself.
The real difference shows up in how Chinese shops handle prototyping and small batches. Western fabricators often charge high setup fees and impose minimum order quantities that force buyers to pay for unused capacity. Chinese foundries aggregate many small jobs onto shared panels, spreading tooling and NRE costs across hundreds of customers. This pooling lets them offer per-unit prices that look impossibly low while still using the same materials—FR-4, ENIG, HASL—specified in the Gerber files. The board you receive isn't thinner copper or skipped testing; it's just riding on an economy of scale that Western job shops can't replicate.
Quality control is another area where assumptions fall apart. Many Chinese suppliers now run automated optical inspection and flying probe tests as standard, not as add-ons. The IPC-A-600 class 2 or class 3 acceptance criteria are the same in Dongguan as in Düsseldorf. What you save isn't from cutting corners on inspection—it's from the fact that a factory running 500 panel designs a week can amortize a $200,000 AOI machine across ten times more boards than a Western shop running 50. The math works because volume drives down fixed costs, not because anyone skips the continuity test.
The Reusable Pattern Advantage That Keeps Tooling Costs Low
Most tooling costs don't come from the initial purchase or build—they pile up through repeated customization and integration. Reusable patterns shift that dynamic by turning one-off solutions into shared team assets. When a toolchain's configuration, scripts, or folder structure gets extracted into a template, the next project doesn't start from scratch. Developers skip the familiarization and trial-and-error phases, directly applying a proven setup instead. That alone removes a significant chunk of the hidden cost that normally accompanies every new initiative.
Beyond the initial savings, reusable patterns centralize maintenance. A fix or upgrade can be rolled out to every project that relies on the pattern, rather than patching each codebase separately. The need for additional tools also drops, since the existing pattern already covers most common scenarios. New tooling only enters the picture when a genuinely novel requirement appears. Over time, this translates into fewer licenses, less onboarding time, and lower context-switching overhead—all without sacrificing flexibility where it actually matters.
Thin Walls and Smooth Finishes That Skip Secondary Machining
Thin walls demand a process that can fill intricate cavities without short shots, while still ejecting parts cleanly. When the tool surface is polished to a mirror finish, the molded or cast part inherits that smoothness directly—no sanding, bead blasting, or hand deburring required. Wall sections down to 0.6 mm stay strong enough for snap-fit assembly because the material flows evenly, eliminating knit lines that often force secondary reinforcement.
Skipping secondary machining isn't just about saving a step; it changes how designers approach tolerance stacks. A housing with a 0.4 mm wall and a molded-in living hinge can arrive at the assembly station with no burrs, no tool marks, and no post-process dimensional drift. This matters most for tight-pack electronics, fluid-handling connectors, and wearable devices where every gram and every surface defect is noticed by the end user.
The real difference comes from controlling fill speed, holding pressure, and cooling rate so the surface replicates the tool exactly. Rather than accepting rough as-molded textures that need rework, targeting Ra 0.4–0.8 μm directly out of the cavity makes sealing ribs and optical windows functional without a single touch from a machine tool.
Where Shell Molding Beats Green Sand and Investment Casting
Shell molding earns its keep when the part geometry demands tighter tolerances than green sand can hold without endless finishing. The resin-coated sand packs against a heated pattern, hardening into a dense, precise cavity that shrugs off the loose, shifting grains that plague traditional sand casting. If you're tired of grinding off thick parting lines or dealing with dimensional drift on medium-volume runs, shell molding simply hands you a cleaner near-net shape right out of the mold.
Against investment casting, shell molding wins on cost and speed for simpler shapes that don't need the fine surface finish of a ceramic shell. Investment casting shines on intricate, thin-walled jewelry or turbine blades, but for brackets, valve bodies, or gear blanks with modest complexity, shell molding cuts out the wax pattern and multiple dip coats. You get a respectable surface smoothness at a fraction of the tooling and cycle time, which is often the deciding factor when you're casting iron or steel in batches of a few thousand.
The real sweet spot sits between the two extremes: parts too precise for green sand but too heavy or too simple to justify investment casting. Shell molding handles thicker walls and larger cores without the cracking risks you see in thin ceramic shells, and it doesn't require the same level of pattern polish. If your foundry is fighting scrap rates or spending too much on secondary machining, switching to shell molding for the right part family can quietly reclaim both margin and floor space.
How to Vet a Chinese Shell Mold Supplier for Consistent Quality
Start by looking past polished sales decks and dive straight into their process control documentation. A supplier that can show you real-time melt temperature logs, shell thickness measurement records from each shift, and a clear traceability system for raw ceramic slurry batches is miles ahead of one that only offers glossy brochures. Ask for the rejection rate data over the last twelve months, not just the final pass rate. If they hesitate or only share summary percentages, that’s a red flag—consistent quality lives in the daily granular details, not monthly averages.
Visit the foundry floor unannounced if possible, or at least insist on a video walkthrough that includes the shell room during active production. Watch how operators handle wax patterns, dip sequences, and drying racks. Look for signs of hurry: uneven stucco application, slurry tanks with floating debris, or racks crammed too tightly for proper air circulation. A supplier that controls humidity and temperature in the drying room with automated sensors—rather than relying on a worker’s gut feeling—will give you far fewer dimensional surprises on the final casting.
Finally, test their willingness to co-engineer quality specs before you place a large order. Send them your most troublesome part geometry and ask for a detailed shell build recipe, including the number of primary coats, backup coats, and recommended dewax autoclave cycle. A good supplier will push back on unrealistic tolerances and propose adjustments based on their own defect history. If they simply agree to everything without asking about your casting alloy, pouring temperature, or post-casting machining plans, you are likely dealing with a trading company that outsources to whoever bids lowest that month.
FAQ
China combines long-standing foundry expertise with modern automated lines, so you get tighter tolerances without the usual cost penalty. Many shops have invested in CNC-machined patterns and rapid induction melting, which trims lead time and improves repeatability.
The resin-coated sand forms a rigid, smooth mold cavity that holds its shape during pouring. This reduces dimensional drift and surface defects, so parts often need less post-machining than those from green sand or basic investment casting.
It can be. Tooling costs are lower than die casting and the shells can be produced quickly on automated equipment. For runs from a few hundred to tens of thousands, the balance of tooling amortization and cycle time often beats alternatives.
Carbon steel, low alloy steel, ductile iron, and stainless steel all respond well because the mold can handle high pouring temperatures. Chinese foundries also frequently cast copper-based alloys for valves and pump bodies.
Ra 6.3 to 12.5 micrometers is common without secondary finishing. With a polished pattern and controlled coatings, some foundries get down to Ra 3.2, especially on flat or gently curved faces.
Many use local silica sand and resin systems, recycle sand aggressively, and run energy-efficient furnaces. This reduces input waste and lets them quote prices that are still competitive for small to medium series.
Deep narrow pockets, sharp internal corners, and very thin ribs can cause mold breakage or fill issues. Adding draft angles and generous radii makes the shell easier to produce and improves yield.
In some cases, yes, especially for complex shapes like gear blanks, levers, and brackets where forging dies would be pricey. Shell mold parts can match surface quality and near-net shape, though forged parts still win for ultimate fatigue strength.
Conclusion
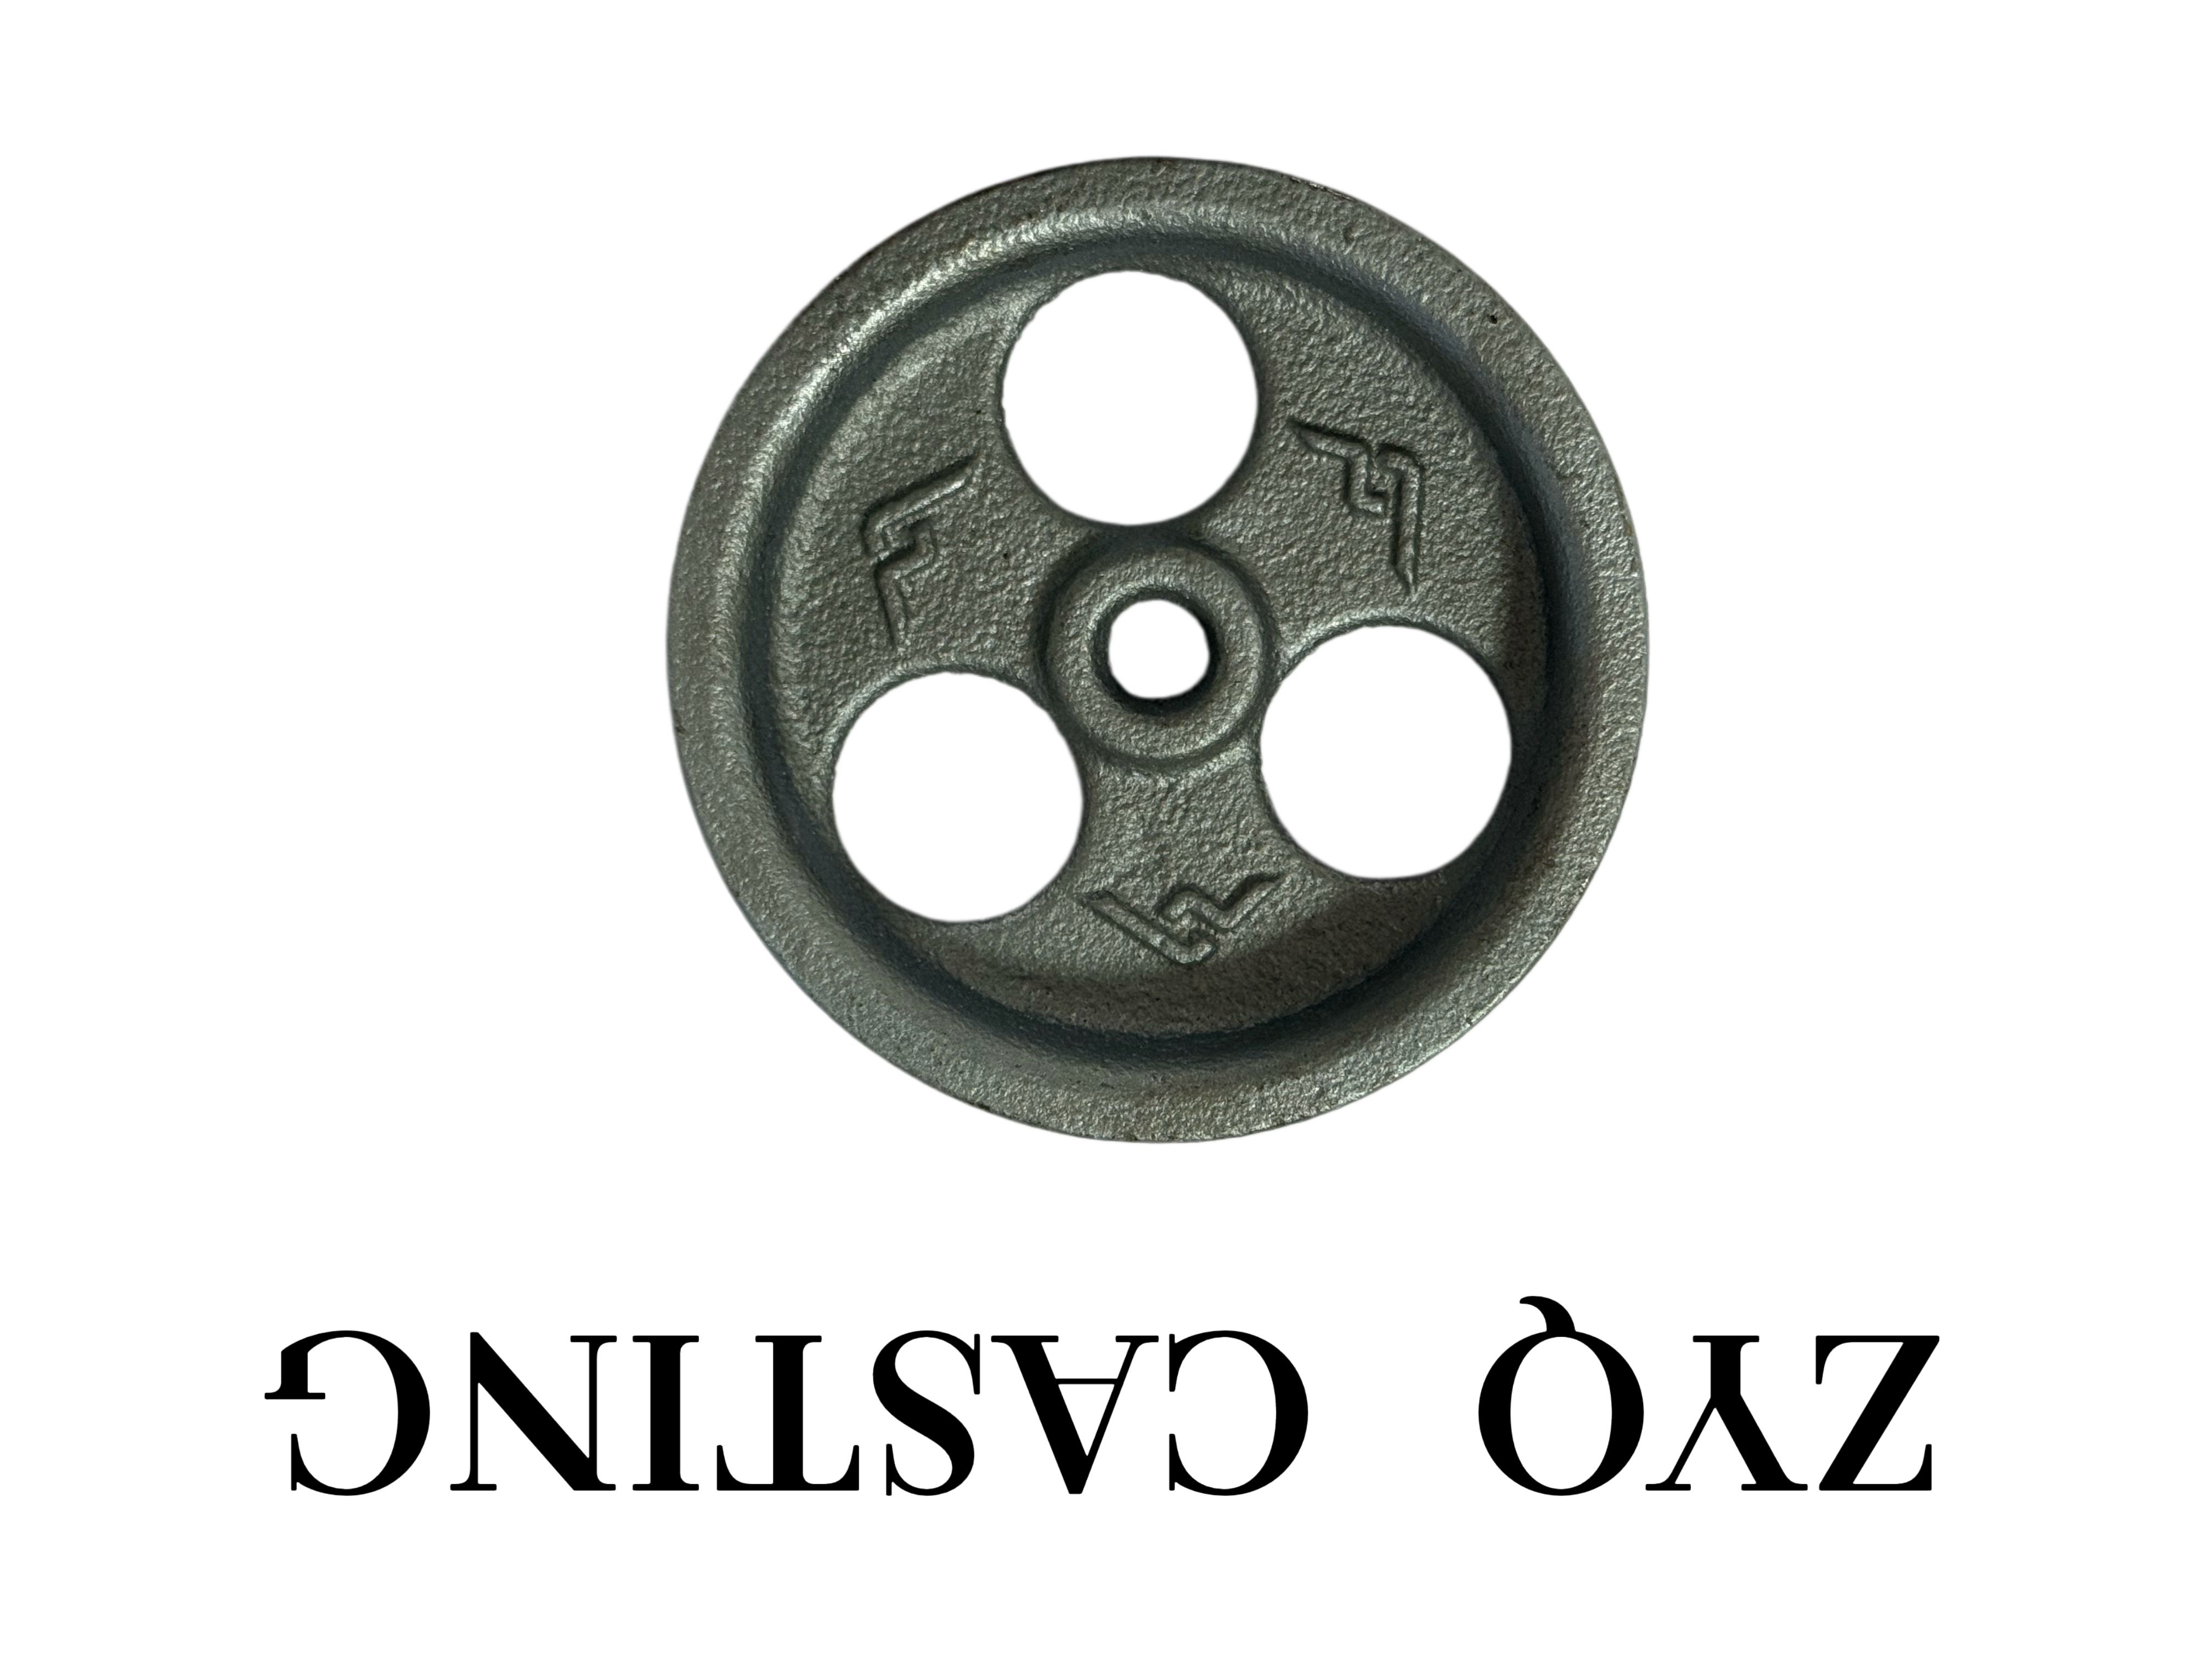
Shell mold casting in China achieves precision through a heat-cured resin-bonded sand shell that hardens against a heated metal pattern, locking in dimensional accuracy before metal pour. The pattern itself is reusable across thousands of cycles, which cuts tooling expenditure compared to one-off investment patterns. Thin-section capabilities down to roughly 2mm and as-cast surface finishes around 60-125 RMS often eliminate secondary machining steps, directly lowering part cost. Chinese foundries maintain these tolerances not by chance but by controlling shell thickness, cure time, and pattern temperature within narrow bands. That tight process control is what separates repeatable shell mold work from inconsistent one-off prototypes.
Price advantages don't come from cheap labor alone. Many Chinese suppliers operate vertically integrated facilities with in-house pattern shops, resin coating lines, and automated shell building, reducing overhead and scrap. Against green sand, shell molding holds tighter dimensions and smoother surfaces without the high wax and shell cost of investment casting, making it ideal for medium-volume precision parts like hydraulic manifolds, gear blanks, and valve bodies. To vet a supplier, buyers should request full dimensional reports for first articles, visit or audit the shell-making area, and confirm raw sand and resin certifications—not just a glossy brochure, because actual process audits reveal whether a shop truly controls sand temperature, cure time, and resin ratios day to day.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/