China Laser Safety Window for Reliable Laser Protection in Industrial Applications
2026-09-24
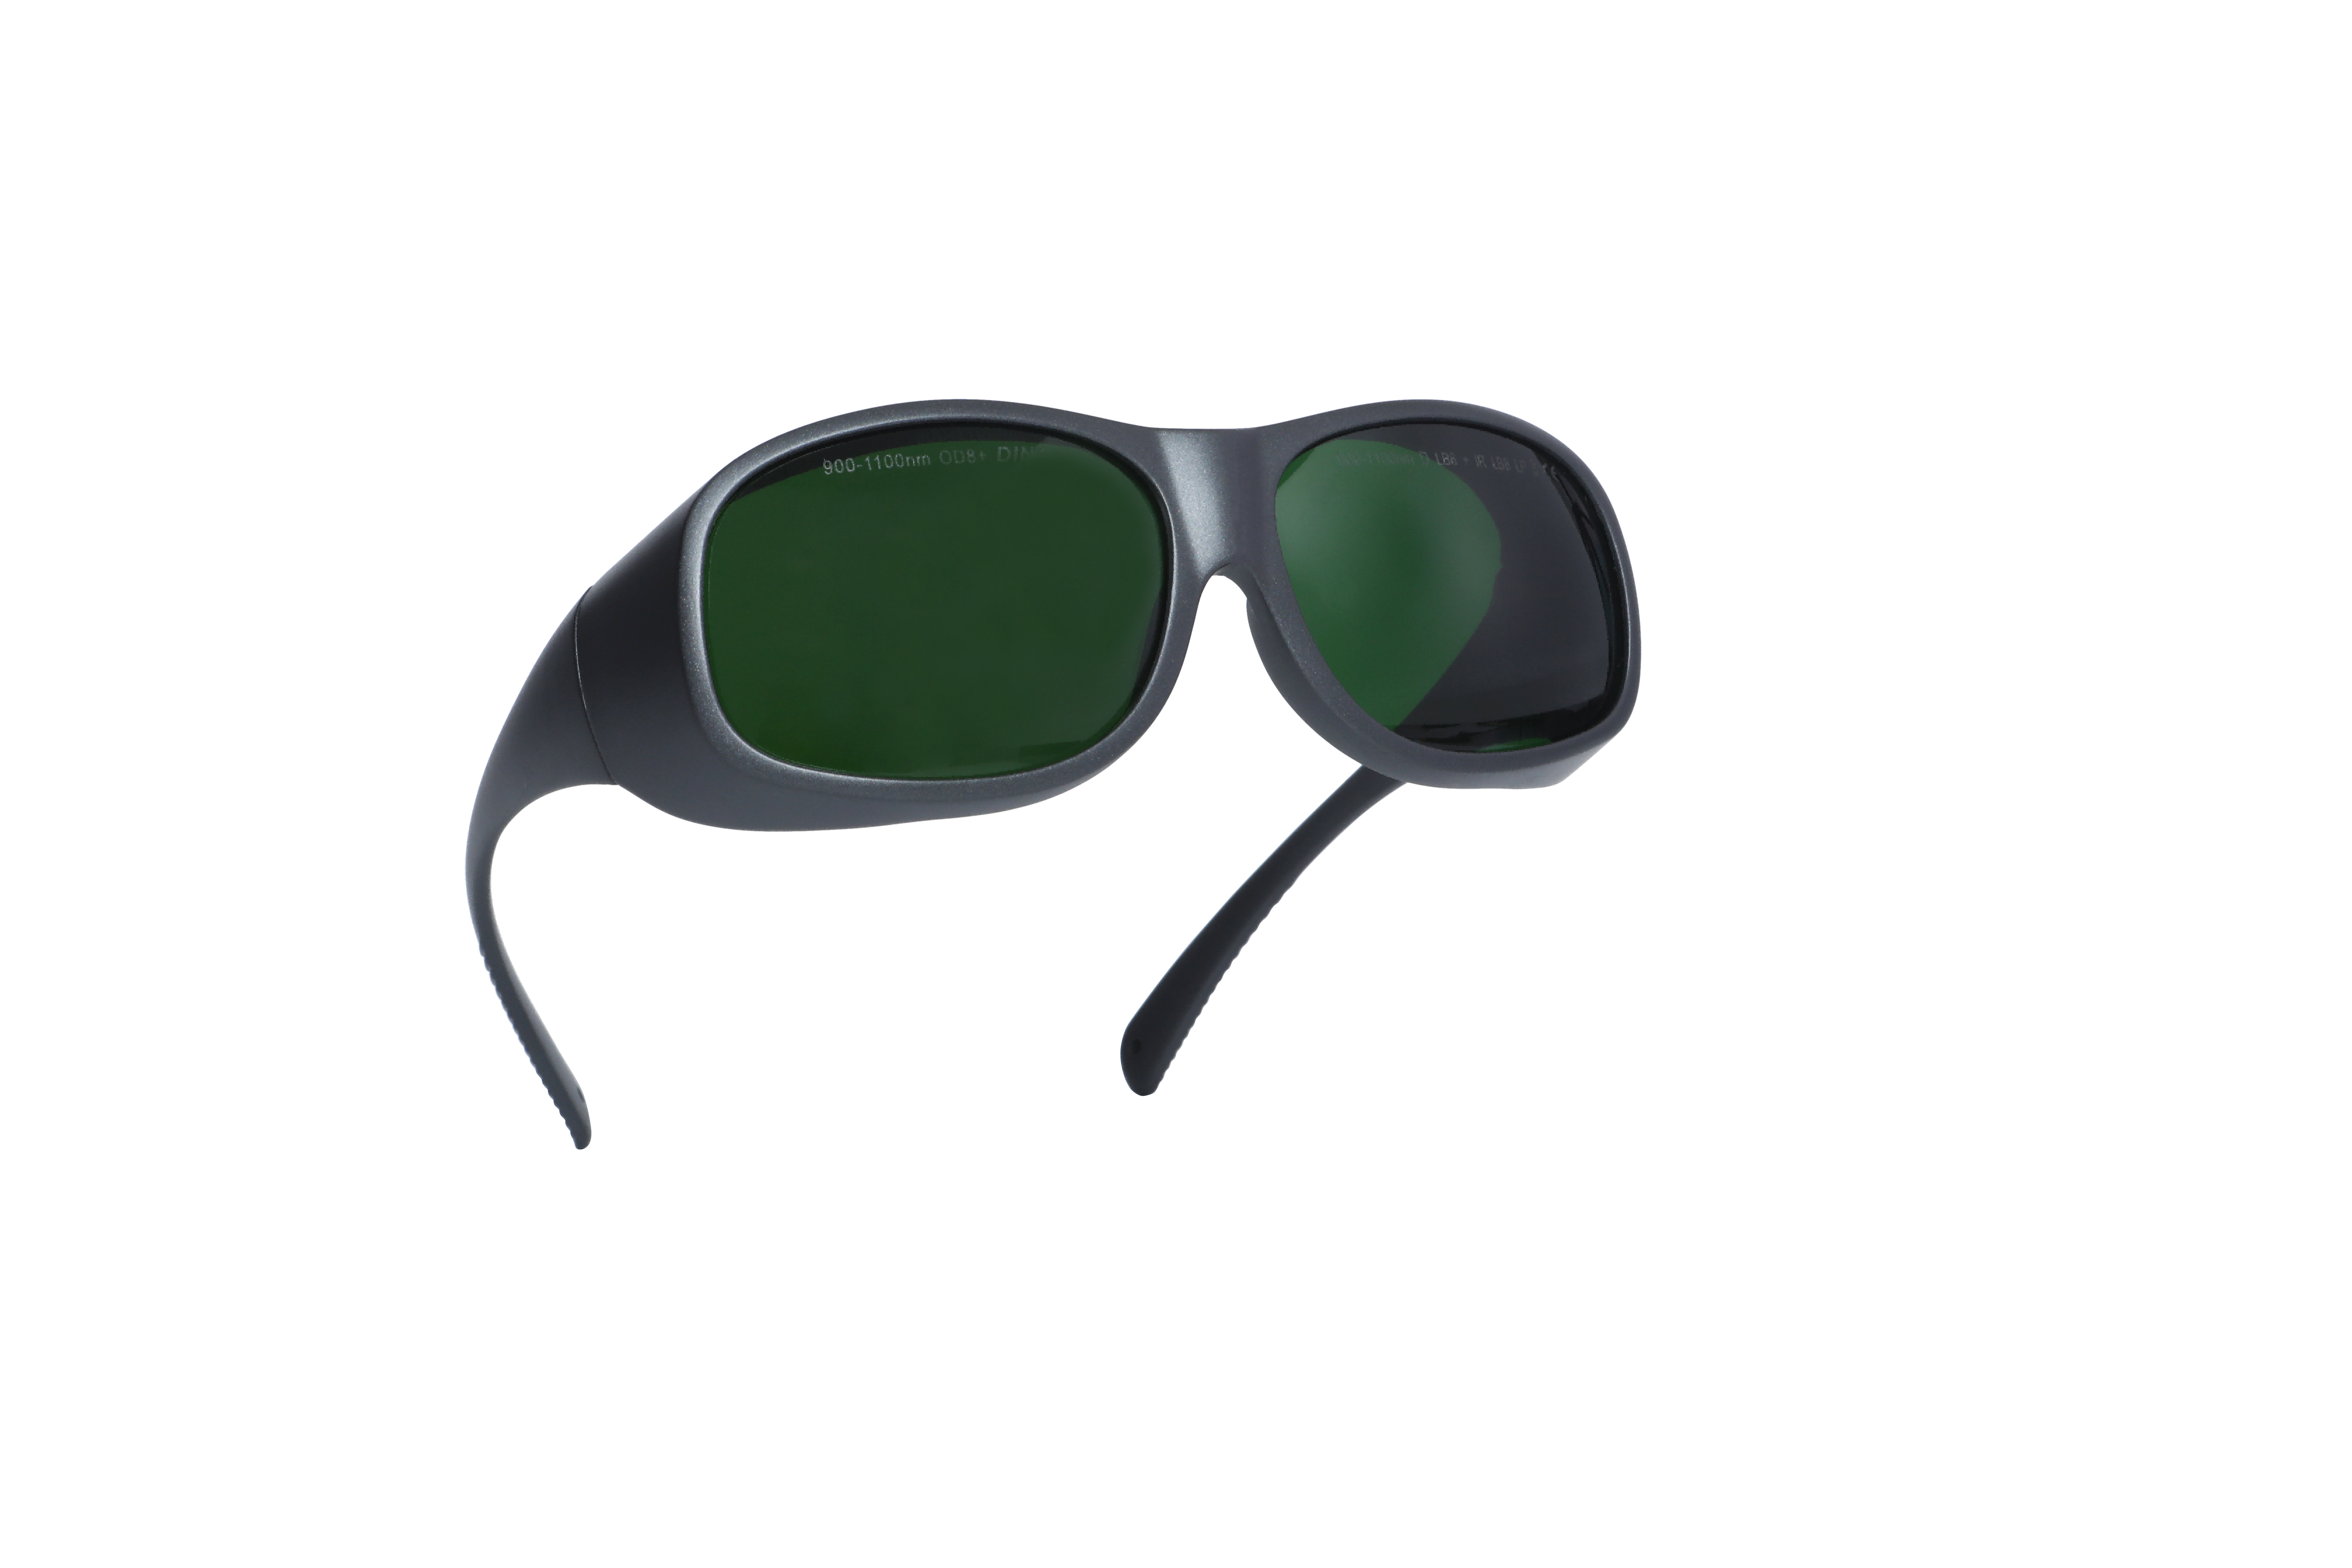
When a laser beam meets an unprotected viewing port, the result is rarely just a close call. For industrial cutting, welding, and engraving operations, a reliable safety window isn't an optional add-on—it's the difference between uninterrupted production and a serious liability. LASERPAIR has focused on exactly this challenge, building China laser safety windows that hold up under real-world conditions. Here's what to look for before you trust any barrier with your operators' eyes and your line's uptime.
Why a Sheet of Green Acrylic Isn't a Laser Safety Window
A green acrylic pane looks like a filter because it's tinted, but tinting alone does nothing to block laser light at specific wavelengths. The green color comes from dyes that absorb some visible light, yet a laser can carry far more energy and may emit at a wavelength that passes right through with little attenuation. Without a measured optical density rating for the exact laser type, the material offers no meaningful protection.
Unlike certified laser safety barriers, ordinary acrylic has no test data for power density, and it can soften, warp, or even ignite under a focused beam. The surface also scatters light unpredictably, so a reflection could bounce toward your eyes or skin. A true safety window is engineered with absorptive or reflective layers matched to the laser's wavelength and power range—not just colored plastic.
People often assume any dark or colored sheet will act as a shield, but laser safety depends on precise optical performance, not appearance. Relying on green acrylic creates a false sense of security, and in a real exposure scenario, it may fail within seconds. The only safe choice is a product rated and labeled for the specific laser system you're using.
Inside Chinese Factories That Test Every Panel Before It Ships
At the end of a panel production line in Shenzhen, the rhythm changes. Conveyors slow nearly to a crawl as each unit passes under a gantry fitted with optical sensors. A worker scans the barcode on the frame, and the screen flashes through a sequence of solid colors—red, green, blue, white, black—while cameras hunt for dead pixels and uneven backlighting. This is not a random audit; it is the standard path for every single panel before it reaches the packing station.
Farther down the line, racks of panels sit inside a burn-in chamber where the temperature holds at 50°C and humidity hovers above 80%. They run looping test patterns for four to six hours, which is enough to expose early failures that would otherwise surface in a customer’s living room. When the chamber doors open, a technician in a cleanroom suit checks each unit under angled light, looking for scratches, dust trapped behind the glass, or a bezel gap wider than a fingernail. The reject bin near the door is rarely empty, but that is the point.
Before packaging, the panel gets one last electrical test: power cycling, signal integrity, and a quick check of the interface ports. The results are written to a database that ties the panel’s serial number to every machine and operator it passed through that day. If a defect pattern spikes, engineers can trace it back to a specific solder paste lot or a mounter nozzle by mid-shift, not weeks later. Testing every panel costs more in labor and equipment, but for these factories it is cheaper than handling returns from overseas and defending a brand against one bad batch.
The Optical Density Numbers That Actually Stop a 10kW Beam
A 10 kW beam doesn’t get stopped by a single magic number. The optical density you need comes from comparing the beam’s power density to the maximum permissible exposure for the relevant wavelength and exposure time. For a near-infrared fiber laser running at 1070 nm with a 1 cm beam diameter, the irradiance is roughly 12.7 kW/cm². If the applicable MPE for a 10-second accidental exposure is around 5 mW/cm², the required attenuation is about 2.5 million times — which translates to an OD of 6.4. Change the beam size or the MPE and the number shifts.
Beam diameter matters more than total power. A 10 kW beam focused down to 5 mm carries almost 51 kW/cm², pushing the required OD to around 7.0 under the same MPE. By contrast, a diffuse 3 cm spot drops the irradiance to about 1.4 kW/cm², and the OD requirement slips to 5.4. That’s why a filter rated OD 6 might block a slow-moving, wide beam but fail catastrophically with a tight focus.
The rating also has to cover the actual wavelength, not just a generic “high power” label. A filter with OD 7 at 1064 nm may be nearly transparent at 532 nm or 10.6 µm. And even if the optical density is mathematically sufficient, the coating or substrate has to survive the incoming fluence. At 10 kW, a filter that attenuates well can still crack, burn, or thermal-lens its way into failure. So the real number is a combination of OD, wavelength match, and damage threshold.
When a Cracked Viewing Window Becomes a Workplace Hazard
A hairline fracture across a viewing window rarely announces itself with a dramatic bang. More often, it begins as a faint spiderweb in the corner of a furnace sight glass or a barely visible scratch on a chemical reactor's observation port. Operators who peer through these windows day after day may grow accustomed to the flaw, treating it as a harmless blemish. But that small crack changes how stress distributes across the glass or quartz surface. A temperature swing, a sudden pressure spike, or even the vibration of nearby machinery can turn a cosmetic imperfection into a sudden, violent failure—sending shards and process media into the workspace.
The hazard isn’t limited to the moment of breakage. A compromised window can leak toxic fumes, superheated steam, or corrosive liquids long before anyone notices a drop in visibility. In food processing, a cracked sight glass might allow cleaning chemicals to seep into product zones. In pharmaceutical manufacturing, a fractured observation window can harbor bacteria in its micro-crevices, undermining sterility. Maintenance teams often underestimate these risks because the window still “looks fine” from a few feet away. Yet the cracks create pathways for contaminants and weaken the barrier that separates workers from high-energy processes.
Recognizing when a cracked viewing window crosses from nuisance to danger requires more than a visual checklist. The type of material matters—borosilicate glass, tempered glass, and quartz each fail differently. The location of the crack relative to gaskets and mounting frames also influences whether the window will hold or blow out. A good rule of thumb is to treat any crack that spans more than a quarter of the window’s diameter, or any crack that grows between inspections, as an immediate lockout-tagout trigger. Replacing a window is cheaper than treating a facial laceration or containing a chemical release. The real workplace hazard isn’t the crack itself—it’s the collective habit of waiting until the glass actually falls out before acting.
Fitting Laser Windows into Robotic Welding Cells Without Gaps
Sealing a laser window into a robotic welding cell isn't just about cutting a hole and bolting on a piece of glass. The real challenge lies in the interface, where hot spatter, fumes, and tiny particulates constantly try to find a way through. Even a half-millimeter gap becomes a path for contamination that degrades optics within days. We approach every installation as a custom fitment task, measuring the cell's wall curvature, frame flex under thermal cycling, and the exact recess depth needed for the window's retaining ring.
The trick is to treat the window not as a standalone component but as part of the cell's pressure envelope. Many fabricators overlook that welding cells often run at slight positive pressure to keep fumes from escaping. A poorly seated window creates a whistling leak that draws dirty air across the laser's protective glass. We use compressible graphite-impregnated gaskets paired with a stepped frame design, so the window compresses into a tapered seat as the clamps are torqued. This removes any visible gap while allowing the stainless frame to expand and contract without stressing the glass.
On retrofits, older cells rarely have square openings. We scan the existing aperture with a handheld laser profiler, then machine the new window frame to match the actual contour, not the nominal drawing. A final light-box test with a 0.05 mm feeler gauge around the entire perimeter confirms zero light leakage before the cell goes back into production. That kind of check catches warpage that would otherwise go unnoticed until the first arc strike fogs the lens.
Cleaning and Inspection Routines That Keep Protection Intact
A quick wipe-down at the end of a shift only knocks off surface dust. The grime that actually breaks down protective layers tends to settle into folds, seams, and adjustment points. Spend a few extra minutes with a soft brush and mild soap on those stress areas, then let everything air-dry away from direct heat. That pause prevents the kind of stiff, cracked material that quietly stops doing its job.
Inspection works best when it happens before the gear goes back on the shelf, not as an afterthought next morning. Run your fingers along straps, buckles, and stitching while the equipment is still in your hands. If a strap no longer holds tension or a buckle shows hairline wear, swap the part now rather than waiting for a visible failure. Small notes in a logbook — date, what was checked, what was replaced — build a record that catches repeat issues early.
FAQ
A rugged frame, scratch-resistant coating, and high optical density across the relevant wavelength range are essential. Industrial environments often expose windows to dust, vibration, and occasional impact, so materials like coated polycarbonate or tempered glass with an abrasion-resistant layer hold up better than standard acrylic.
The filter uses absorptive dyes or reflective coatings that target specific laser wavelengths while allowing a useful portion of visible light through. The result is a window that looks relatively clear or lightly tinted but still attenuates the dangerous beam to safe levels, keeping operators able to see the work area.
Stock options usually cover common industrial lasers such as Nd:YAG at 1064 nm, fiber lasers around 1070 nm, CO2 lasers at 10.6 µm, and diode lasers from 800 nm to 980 nm. Optical density ratings typically range from OD4 to OD7, with OD6 being a frequent choice for high-power cutting and welding systems.
Look for compliance with EN 60825-4 or ANSI Z136.7, which cover laser protective barriers and windows. CE marking is expected for products sold in Europe, and a test report from an independent lab confirming the optical density and damage threshold adds confidence.
Yes, most Chinese suppliers offer custom dimensions, edge finishing, and even pre-drilled mounting holes. Lead times for custom sizes are often shorter than many buyers expect, but it is wise to confirm the maximum size limit and minimum order quantity before committing.
Many factories in China have invested in automated coating and lamination lines, which keeps consistency high while reducing cost. Lead times for standard windows can be as short as one to two weeks, while custom orders may run three to five weeks depending on the optical density and substrate.
Dust and debris can scatter laser light and create hot spots, so clean the window regularly with a soft microfiber cloth and a mild, ammonia-free cleaner. Avoid paper towels and aggressive solvents, as they can scratch the surface or degrade the coating, reducing both clarity and protection.
Glass offers better scratch resistance and higher thermal stability, making it a safer choice near high-power beams or where sparks are common. Polymer windows, usually acrylic or polycarbonate, are lighter and easier to cut into custom shapes but may need more frequent replacement in abrasive or high-temperature settings.
Conclusion
A sheet of green acrylic might look like a laser safety window, but in an industrial environment where a 10kW beam is present, appearance means nothing. Chinese suppliers that take laser protection seriously run every panel through a bench test before it ships, checking optical density at the exact wavelength of the laser in use. That OD number is not a marketing detail—it is what stands between an operator and permanent eye damage. Without a verified OD rating matched to the laser's power and wavelength, even a thick transparent panel can transmit enough energy to cause harm in a fraction of a second.
Once installed, the window becomes part of a robotic welding cell, so the fit has to be gap-free; any opening around the frame lets stray reflections escape. A cracked viewing window is not a minor cosmetic issue either. Stress from heat, spatter, or impact can turn a hairline fracture into a failure point that scatters or passes the beam. Regular cleaning and inspection routines matter just as much as the initial specification. Using approved cleaners, checking for surface damage, and replacing panels before they degrade keeps the protection intact and keeps the production line running without surprises.
Contact Us
Contact Person: Jenny
Email: [email protected]
Tel/WhatsApp: +86 13537713281
Website: https://www.laserpair-safety.com/